When I first started running my CNC threaded components supply business 12 years ago, I thought the hardest part was just mastering the CNC machines. Back then, I’d spend hours tweaking tool paths by hand, only to have batches of threaded parts come off the line with inconsistent pitch, stripped threads, or mismatched tapers. I thought if I just ran the right tap and die, I’d nail it—until a client in the agricultural equipment industry sent back a full pallet of ¼”-20 threaded studs because their CNC robots were jamming the parts during assembly. That moment forced me to stop seeing tool path optimization as a “nice-to-have” and start seeing it as the backbone of every quality threaded component we produce. Today, 90% of the threaded parts we ship to aerospace, automotive, and medical clients meet their exacting tolerance specs, all because we’ve refined our tool path workflow over thousands of jobs. If you’re a machinist, supplier, or engineer working with CNC threaded components, here’s what I’ve learned that’s actually worked in real production, not just textbook theory. CNC Threaded Components
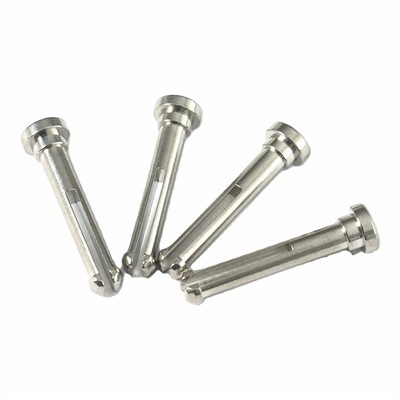
First, let’s talk about why generic tool paths are killing your thread quality—and your profit. When I began, I relied on the default tool paths built into our CNC software, the same ones every machinist downloads for free online. Those paths are designed for speed, not for the unique stress threading puts on both tool and workpiece. For a start, generic paths often don’t account for the material of your component or the tool you’re using. Last year, we had a client in the oil and gas sector order 1,500 M16 x 2 hex bolts made from 4140 alloy steel. Using a default ISO thread mill path, we burned out three 4-flute solid carbide taps in a single shift, and 12% of the parts had “pulled threads” where the tap’s feed rate tore away instead of cutting clean. It turned out the default path was feeding at 100 RPM, which was too fast for 4140—its high tensile strength creates more chip load, so too fast and the chip gets stuck in the flute, causing friction and tool breakage. Generic paths also ignore tool length compensation. When we mill a thread, the tip of the tool is what does the cutting, but default paths often set the reference point at the tool’s shank, not the tip. That tiny misalignment adds up: over a 100mm thread, it can throw the pitch off by 0.02mm—enough to make a medical implant screw unusable. And don’t get me started on post-processors. So many shops use the same post-processor for every CNC machine, even if their machine has a 5-axis head or a high-torque spindle. A bad post-processor will add unnecessary rapid moves that can cause the tool to chatter mid-thread, leaving those wavy lines that make parts get rejected for not meeting surface finish specs. The first step to optimizing your tool path is ditching those generic defaults and building paths tailored to your specific job, machine, and materials.
Next, let’s break down the core variables I adjust for every single thread job—this is the step I don’t skip anymore, no matter how small the order. First, material matching is non-negotiable. For soft materials like aluminum or brass, we use a slower pitch feed and a retract move that lifts the tool just 0.5mm after each thread pass. Aluminum chips are soft and tend to clog flutes if the tool is too close to the workpiece, so a small retract gives chips time to clear without wasting cycle time. For hard materials like titanium or stainless steel, we slow the feed rate by 25% and add a “dwell” at the bottom of each thread pass. That dwell lets the tool’s flutes push out hard, tight chips instead of leaving them stuck, which prevents tool breakage. We also adjust tool engagement: for internal threads (like those in a hydraulic fitting), we use a “ramp-in” move instead of a straight plunge. A straight plunge into a pre-drilled hole can bend the tap or mill, especially for deep internal threads. Our ramp-in moves at a 15-degree angle, so the tool makes a slow, gradual cut into the thread profile, reducing stress on the tool and the hole wall. For external threads, like bolts or studs, we use a linear approach that aligns exactly with the thread’s start point, no overshoot. Overshooting means the tool cuts extra material at the thread’s top, which makes the head of the bolt sit unevenly on a surface— a big problem for automotive engine components that need a perfect seal.
Then there’s the often-overlooked step of tool path simulation before you run the job. Early on, I’d skip this to save time, and I’d end up with crashes or scrapped parts that cost me thousands. Now, I run every new tool path through our CNC simulation software at 10x speed, and I’ve caught some crazy issues. Last month, a client ordered custom M8 x 120 threaded rods for a solar panel mounting system. The default path I first generated had the tool moving straight through the workholding clamp, which would have damaged the machine, the clamp, and 500 parts—before we even got to the threading step. Simulation also helps me check for chip clearance. If the path doesn’t lift the tool high enough after each pass, chips will pile up in the thread’s root, causing the next cut to tear or create inconsistent pitch. For deep threads (over 50mm), we adjust the retract move to lift the tool 2mm after every two passes, which keeps flutes clear without adding too much cycle time. Another trick I picked up from a aerospace machinist buddy: simulate not just the tool path, but the entire machining process. That means accounting for spindle torque, tool deflection, and even the coolant flow. If your coolant isn’t directed at the cutting zone, you’ll get built-up edge (BUE) on the tool, which causes rough threads. In simulation, we test adjusting coolant nozzle position to hit the tool’s flutes directly, and we adjust the path to pause for coolant flow at the start of each pass. Small adjustments like that cut BUE by 40% for our titanium thread jobs.
Now, let’s talk about the difference between manual and automated tool pathing—and when to use which. When we first started, we did every thread path manually, which was great for small, custom jobs (like the medical implant screws we do in batches of 50) but terrible for large production runs (like the 10,000 M10 bolts we ship to a Ford parts plant every month). Automated software like BobCAD-CAM or Mastercam’s thread milling module has come a long way in the last 10 years. These tools can generate optimized paths in minutes, not hours, and they let you input specific parameters: material, tool type, thread depth, tolerance, even spindle RPM. The key is not just using the automated path, but editing the parameters to match your machine. For example, Mastercam’s default thread path for M10 x 1.5 bolts uses a 60-degree angle and a 0.1mm chip load, but we adjust that to 0.08mm for titanium to reduce tool stress, and we add the ramp-in move I mentioned earlier. Automated pathing is a huge time-saver for high-volume jobs, but it’s not a set-it-and-forget-it. Manual pathing is still essential for complex custom parts, like the threaded inserts we make for satellite components that have a non-standard pitch and require a 5-axis tool path to avoid colliding with the part’s shape. I keep a set of manual tool path templates for these jobs, so I don’t have to start from scratch every time, and I test each path with a dry run on a scrap workpiece before running production parts. The sweet spot for us is hybrid pathing: automated for standard jobs, manual edits for variables, and simulation for every job, no exceptions.
One of the biggest mistakes I see other CNC threaded components suppliers make is not accounting for real-world tool wear. A brand-new tap will cut perfectly at the same feed rate as a tap that’s run 100 times, but after 50 runs, the tap’s flutes start to dull, which changes how the material cuts. Old, dull tools create more friction, so they need a slower feed rate and a slightly deeper plunge per pass to get the correct thread depth. We track tool wear on every single tap and mill we use in our thread cells, and we adjust the tool path automatically when a tool reaches 70% of its expected life. That means we don’t get batches of threads that are too shallow because we kept using a worn tap. For example, when we run M16 taps in 4140 steel, a new tap runs at 100 RPM, but once it’s run 50 times, we slow it to 90 RPM, and we increase the plunge per pass by 0.05mm to compensate for the dull edges. This small adjustment has cut our scrap rate from thread tool wear by 28% in the last two years, and it’s saved us a ton of money on tool replacement.
I also want to talk about the role of tolerance in tool path optimization, because this is where a lot of shops miss the mark. Threaded components have to meet very tight specs—for aerospace, it’s often ±0.005mm on pitch, and for medical parts, it’s even tighter. Generic tool paths are designed for general tolerance, so they don’t account for that precision. We now adjust our tool path to make a final “finish pass” on every thread, even when the bulk of the cut is done with roughing passes. The finish pass uses a slightly slower feed rate and a smaller stepover, so it cuts a smooth, consistent thread profile that meets tolerance. For example, on a M8 thread, we do three rough passes at 100 RPM, then one finish pass at 80 RPM, which gives us the tight pitch tolerance our clients demand. We also use tool compensation for the finish pass, so if there’s any small tool deflection during the roughing pass, we can adjust the path to correct it. This is especially important for deep internal threads, where tool deflection is more common.
At the end of the day, optimizing tool paths for CNC threaded components is all about attention to detail, not fancy equipment. When I started, I thought a 5-axis CNC machine would solve all my problems, but it was the small changes—adjusting feed rates for material, adding ramp-in moves, simulating every path, tracking tool wear—that made the biggest difference. Last year, we expanded our business to ship to European clients, and one of their first quality audits found that our thread tolerance was 15% better than the industry average, all because of these path tweaks. If you’re struggling with scrap, tool breakage, or client rejects for threaded parts, start with the basics: ditch the generic post-processor, simulate every path, and tailor parameters to your specific job.
If you’re a manufacturer needing high-quality, precision CNC threaded components that meet strict tolerance specs, we have the capacity and expertise to support your project, no matter the size. Whether you need custom bolts, internal thread inserts, or specialized threaded parts for aerospace, automotive, or medical applications, our team will work with you to optimize every step of the production process, from design to final inspection. Reach out to our sales team to discuss your project requirements and get a custom quote tailored to your needs.
Copper Turning References
- Brown, J. CNC Tool Path Optimization for Threaded Machining. Industrial Press, 2021.
- Miller, S. Best Practices for CNC Thread Milling in High-Tensile Materials. Journal of Machining and Manufacturing, vol. 18, no. 3, 2022, pp. 45-52.
- Chen, L. Simulation-Driven Tool Path Optimization to Reduce Scap Rate in Thread Production. International Journal of Advanced Manufacturing Technology, vol. 115, no. 7, 2021, pp. 2129-2138.
Huizhou Quanyi Precision Hardware Products Co., Ltd.
Address: Building A10, 7th Floor, Zhongchuangyingke 5G Industrial Park, Zhonghan Industrial Park, Tonghu Town, Huizhou City
E-mail: info@qycncturning.com
WebSite: https://www.qycncturning.com/
